The global push toward smarter electrical manufacturing is reshaping how miniature circuit breakers are produced. The International Federation of Robotics reported 541,302 new industrial robots installed worldwide in 2023. Asia accounted for most installations, with China remaining the largest market. These figures show strong automation demand, but they do not guarantee reliable MCB production.
A capable Mcb Assembly Robot must do more than place components quickly. It should manage spring loading, contact installation, screw fastening, electrical testing, and final inspection with repeatable accuracy. Buyers should examine cycle time, torque control, vision performance, changeover design, and production traceability. Small errors matter. A poorly seated terminal can create costly rejects or safety concerns.
Standards matter too. IEC 60898-1 guides requirements for household and similar circuit breakers, while ISO 10218 supports industrial robot safety practices. Reputable manufacturers explain how their systems support these requirements. They also provide validation records, spare-parts planning, operator training, and responsive technical service.
This guide evaluates leading MCB assembly robot manufacturers for global buyers. It considers engineering capability, integration experience, quality systems, and after-sales support. Factory demonstrations can be useful. Yet demonstrations may hide difficult realities, such as mixed product models, unstable component feeding, or lengthy maintenance.
Look beyond speed.
The best supplier is not always the cheapest or most automated. A practical assessment should compare verified production results, total ownership costs, safety documentation, and local support. Industry reports offer valuable context, but each factory still requires careful technical review. That step is often underestimated.
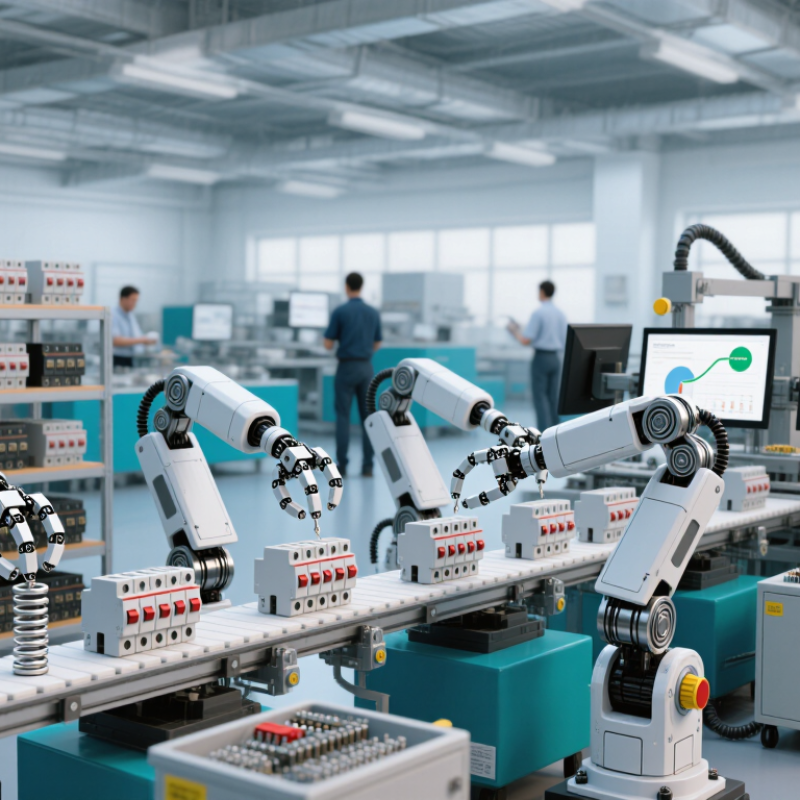
MCB assembly robots support the production of miniature circuit breakers through controlled, repeatable operations. They handle small components, reduce manual handling, and maintain stable cycle times. Their scope covers component feeding, mechanism assembly, terminal installation, screw fastening, and electrical testing. In a well-designed line, each station records process data for later review. This matters.
Core manufacturing functions include precise part picking, contact placement, spring installation, and housing closure. Robots can insert arc chutes and trip mechanisms without damaging delicate surfaces. Servo-driven tools control fastening torque and help prevent loose terminals. Vision systems check component orientation, missing parts, and visible assembly defects. Electrical stations may verify continuity, insulation performance, and trip response under controlled conditions. Traceability software links test results to production batches.
During supplier evaluations, I look for stable tooling, accessible maintenance points, and clear fault messages. A reliable manufacturer should explain cycle time using real component samples, not only laboratory figures. Operators still need training for changeovers and unusual defects. That part is often underestimated. Automation is not a cure-all. Poorly calibrated sensors can create false rejects, while weak feeding systems cause repeated stoppages. The better approach combines robotic precision with practical human oversight, documented inspections, and regular process reviews.
Automated MCB assembly systems combine precision feeding, robotic handling, fastening, and inspection. Vibratory or flexible feeders orient small components such as springs and terminals. Cameras check their position before a robot places them. A misplaced spring can affect later assembly, so reliable part presentation matters as much as robot speed.
Servo-driven stations control screw tightening and record torque values for each unit. Some lines use specialized joining processes for electrical contacts, while calibrated stations verify trip mechanisms and operating clearances. Machine vision can detect missing parts, skewed components, or surface defects under consistent lighting. Then electrical test stations check performance against defined production specifications. Small details count.
The most useful systems connect these steps through a programmable line controller and production data records. This helps engineers trace a failed test to a station, batch, or process setting. Yet automation is not automatically reliable. Dust, reflective metal, and component variation can confuse sensors, and rushed changeovers may introduce new errors. Good commissioning includes repeatable trials, clear maintenance routines, and operator training. Even then, some edge cases appear only after months of production. A practical design leaves room for adjustment, rather than assuming every component behaves perfectly.
Top MCB Assembly Robot Manufacturers for Global Buyers
How to Evaluate MCB Assembly Robot Manufacturers Globally
Global robot demand gives useful context. The International Federation of Robotics reported 541,302 industrial robot installations in 2023, with more than 4.28 million robots operating worldwide. However, broad automation growth does not prove MCB assembly competence. Buyers should examine proven experience with miniature circuit breaker production, including contact insertion, spring placement, screw fastening, label application, and electrical testing.
Ask manufacturers for measurable results from comparable projects. A reliable supplier should provide cycle-time records, first-pass yield, torque-control accuracy, and fault-recovery data. For example, request a live demonstration using your housing, terminals, and springs. Watch the machine handle a misaligned component. Small details matter. Also verify traceability, vision-system resolution, changeover time, and spare-part availability in your region. The International Federation of Robotics World Robotics 2024 report can support general robotics benchmarking, but it cannot replace application-level testing.
Safety and integration require equal attention. Check compliance with ISO 10218 for industrial robot safety and request documented risk assessments. Review factory acceptance testing, site acceptance testing, operator training, and maintenance instructions. A manufacturer claiming 24-hour operation should show downtime logs, not only polished videos. Some suppliers publish impressive output figures without explaining rejection rates. That deserves scrutiny. I would also question overly precise payback promises, because labor costs, product variants, and local service response can change the calculation. A practical evaluation should include sample production, ten consecutive hours of testing, and direct discussion with engineers who built the control software.
| Top MCB Assembly Robot Manufacturers for Global Buyers - How to Evaluate MCB Assembly Robot Manufacturers Globally | |||
|---|---|---|---|
| Evaluation Dimension | What to Assess | Evidence to Request | Practical Verification |
| MCB Process Experience | Experience with the specific miniature circuit breaker (MCB) design, rated-current range, product variants, and required assembly operations. | Process flow, sample application records, equipment scope, and a list of included and excluded operations. | Review a process map from component feeding through assembly and end-of-line testing. Confirm which steps are automated and which require manual handling. |
| Process Coverage | Ability to integrate relevant operations such as component feeding, assembly, riveting, contact joining, calibration, testing, marking, and packaging where required by the product. | Station layout, equipment list, tooling scope, and description of the proposed automation sequence. | Compare the proposed line scope with the buyer’s product and process requirements. Confirm interfaces between stations and identify any outsourced or separately supplied equipment. |
| Product and Standard Alignment | Understanding of the applicable product requirements. IEC 60898-1 covers circuit-breakers for overcurrent protection for household and similar installations; IEC 60947-2 covers low-voltage circuit-breakers. | Written statement of the standards and product specifications considered in the design, plus the planned test methods. | Have the buyer’s engineering and compliance teams confirm which standard and edition apply to the intended product and market. Do not treat a machine supplier’s statement as product certification. |
| Assembly and Calibration Control | Control of critical assembly parameters, calibration adjustments, recipe management, and prevention of incorrect settings or component mix-ups. | Control plan, parameter list, recipe-change procedure, and examples of alarm and interlock logic. | Run representative product variants and verify that the system selects the correct recipe, records relevant settings, and blocks unauthorized or invalid changes. |
| End-of-Line Testing | Test coverage appropriate to the product specification, such as electrical checks and functional or trip-characteristic tests where required. | Test-station specifications, measurement equipment details, calibration records, test limits, and sample test reports. | Review test limits against the approved product specification. Confirm how failed units are identified, rejected, and prevented from being recorded as passing. |
| Traceability and Data | Recording of the production and test information required for quality investigations, including product identification, results, timestamps, and relevant process parameters. | Sample data records, data-field list, export formats, retention options, and interface documentation. | Trace a sample unit from its identifier to its recorded assembly and test results. Confirm data export and recovery procedures with the buyer’s IT team. |
| Changeover and Flexibility | Time and steps needed to change between approved MCB variants, including change parts, software recipes, and operator actions. | Changeover procedure, list of format parts, supported product matrix, and any stated changeover-time assumptions. | Witness a changeover between representative variants. Check setup verification, first-piece approval, and safeguards against using the wrong parts or recipe. |
| Robot and Machine Safety | Risk assessment and safety measures for the integrated machine, including robot access, guarding, interlocks, emergency stops, and safe maintenance access. | Risk assessment, safety-system design information, electrical documentation, and validation records for safety functions. | Review the design against applicable requirements, including ISO 12100 for machinery risk assessment, ISO 10218 for industrial robot safety, and ISO 13849-1 where relevant to safety-related control systems. |
| Machine Electrical and Integration Design | Electrical design, control architecture, plant-interface requirements, and compatibility with the buyer’s utilities and factory systems. | Electrical schematics, utility requirements, I/O list, interface specifications, and the proposed controls architecture. | Check the electrical documentation and integration scope against the installation site. Review applicable machinery electrical requirements, including IEC 60204-1. |
| Capacity and Performance Claims | Output claims stated with clear assumptions about product mix, operating pattern, staffing, changeovers, and planned downtime. | Cycle-time study, capacity calculation, acceptance-test definition, and any stated performance exclusions. | Measure output during a buyer-witnessed production run using the agreed product mix and acceptance criteria. Separate demonstrated results from estimates. |
| Factory and Site Acceptance | Defined acceptance stages for the machine before shipment and after installation, with agreed responsibilities and pass/fail criteria. | Factory Acceptance Test (FAT) and Site Acceptance Test (SAT) plans, test records, punch lists, and completion criteria. | Agree in advance on sample products, test duration, quality checks, data review, and resolution of open items before shipment and final handover. |
| Documentation and Training | Completeness of operating, maintenance, troubleshooting, safety, and spare-parts documentation, plus training for relevant personnel. | Documentation index, sample manuals, training agenda, language options, and handover checklist. | Confirm that manuals and training materials are available in the required languages and cover normal operation, changeover, fault recovery, and safe maintenance. |
| Service and Spare Parts | Availability of technical support, spare parts, remote assistance, and escalation procedures for the buyer’s production location. | Service coverage description, support channels, spare-parts list, recommended inventory, and service-level terms. | Confirm support hours, response commitments, shipping arrangements, warranty conditions, and the process for diagnosing production stoppages. |
| Commercial and Delivery Scope | Clarity of the quotation, project schedule, installation responsibilities, exclusions, payment milestones, and change-control process. | Itemized quotation, delivery schedule, scope matrix, assumptions, warranty terms, and proposed project-change procedure. | Compare bids using the same scope and acceptance criteria. Record any buyer-supplied items, site work, taxes, logistics, and commissioning exclusions. |
MCB assembly robot suppliers usually fall into three practical categories: dedicated automation builders, electrical equipment manufacturers, and contract engineering firms. Each category serves a different purchasing priority. Dedicated automation builders often design flexible cells with screwdriving, terminal insertion, testing, and vision inspection. Electrical equipment manufacturers may offer tighter process integration and better product knowledge. Contract engineering firms can adapt standard modules for unusual layouts or mixed production.
Regional strengths Regional strengths shape the buying decision. European manufacturers are often valued for precision, traceability, and mature safety engineering. Their systems may suit plants requiring detailed process records and stable quality controls. East Asian suppliers commonly provide strong production capacity, fast component sourcing, and competitive system costs. They are useful for high-volume MCB lines, especially when cycle time matters. North American integrators often focus on custom controls, retrofit work, and responsive technical support. Southeast Asian suppliers are gaining attention for assembly capacity and practical labor-saving solutions.
What to verify before buying Factory experience shows that the cheapest quotation is rarely the simplest choice. A low initial price may hide limited training, spare-part delays, or difficult software changes. I have seen promising projects slow down because the robot cell was not tested with real component tolerances. Regional reputation helps, but it does not replace a witnessed factory acceptance test. Ask about cycle-time evidence, reject handling, maintenance access, and operator training. Small details matter. Some suppliers still underestimate future product variations, and buyers should challenge that assumption before signing.
Selecting an MCB assembly robot manufacturer requires more than comparing hourly output. Global buyers should inspect engineering records, factory references, and service capacity in the destination region. Ask for sample assemblies using your actual breaker housings, terminals, springs, and labels. A polished demonstration is not enough.
Integration details often decide project performance. Confirm feeder orientation, screwdriving torque, vision inspection, reject handling, and traceability before signing. Request cycle-time data under realistic conditions, including material changes and minor stoppages. The control system should exchange data with production software through documented interfaces. Safety design should address guarding, emergency stops, access doors, and safe maintenance procedures. Factory acceptance testing and site acceptance testing need measurable pass criteria.
Compliance cannot be added casually after installation. The machine builder should provide risk assessments, electrical schematics, manuals, and conformity documentation suitable for the target market. Product testing may involve applicable circuit-breaker standards, while machinery requirements can include functional safety and electromagnetic compatibility. Requirements differ by country. Confirm them with an accredited testing body or qualified local engineer. It is easy to assume one certificate covers every market. It often does not.
Purchasing teams should also review spare-part availability, operator training, software backups, and response times. Keep payment milestones linked to verified deliverables. A lower quotation may conceal tooling limits or expensive integration work. That lesson is uncomfortable, but useful. Some uncertainty will remain, especially with new component designs, so a pilot run is worth budgeting for.
Content © 2025 Komatsu. All Rights Reserved